Best Air Slip Ring Solutions for Reliable Rotational Connectivity
2026-09-21
What if your rotating equipment could transfer air, gases, or vacuum without a single leak—even at high speeds? That’s the promise of a well-engineered air slip ring, and it’s a bigger deal than most engineers realize. Whether you're designing automated packaging lines, wind turbines, or rotary tables, unreliable rotary unions lead to pressure drops, downtime, and costly maintenance. In this guide, we’ll break down what separates a truly reliable air slip ring from the rest, and why MOFLON has become a go-to name for demanding rotational connectivity. From custom channel counts to mixed media integration, you’ll discover practical insights to help you choose the best solution for your next project.
Why a Perfect Seal Matters More Than Fancy Housing
A product's outer shell is what people notice first, but the real test of durability happens at the seam where two parts meet. A beautifully finished housing can still let in moisture, dust, or air if the seal underneath is poorly chosen or badly installed. The housing is essentially a frame; the seal is the working barrier. Once that barrier fails, no amount of surface polish or premium material on the outside will restore the internal protection.
Seals also have to handle conditions that the housing itself never directly faces. Temperature swings cause materials to expand and contract at different rates, and a seal must keep contact pressure through every cycle. Vibration, pressure differentials, and rough handling all concentrate stress at the interface. A casing can be rigid and impressive, but if the seal loses compression set or cannot follow surface irregularities, the system is no longer closed. That is why a modest-looking housing with a correctly specified seal will often outlast a flashy enclosure with an average one.
Over time, the gap between a perfect seal and a mediocre one shows up in ways that matter: fewer failures, less contamination, and consistent performance without constant retightening or replacement. A fancy housing may win the first impression, but the seal is what preserves function long after the unboxing thrill is gone. It is the quiet detail that keeps everything else working.
What High-Speed Rotation Does to Internal Air Channels
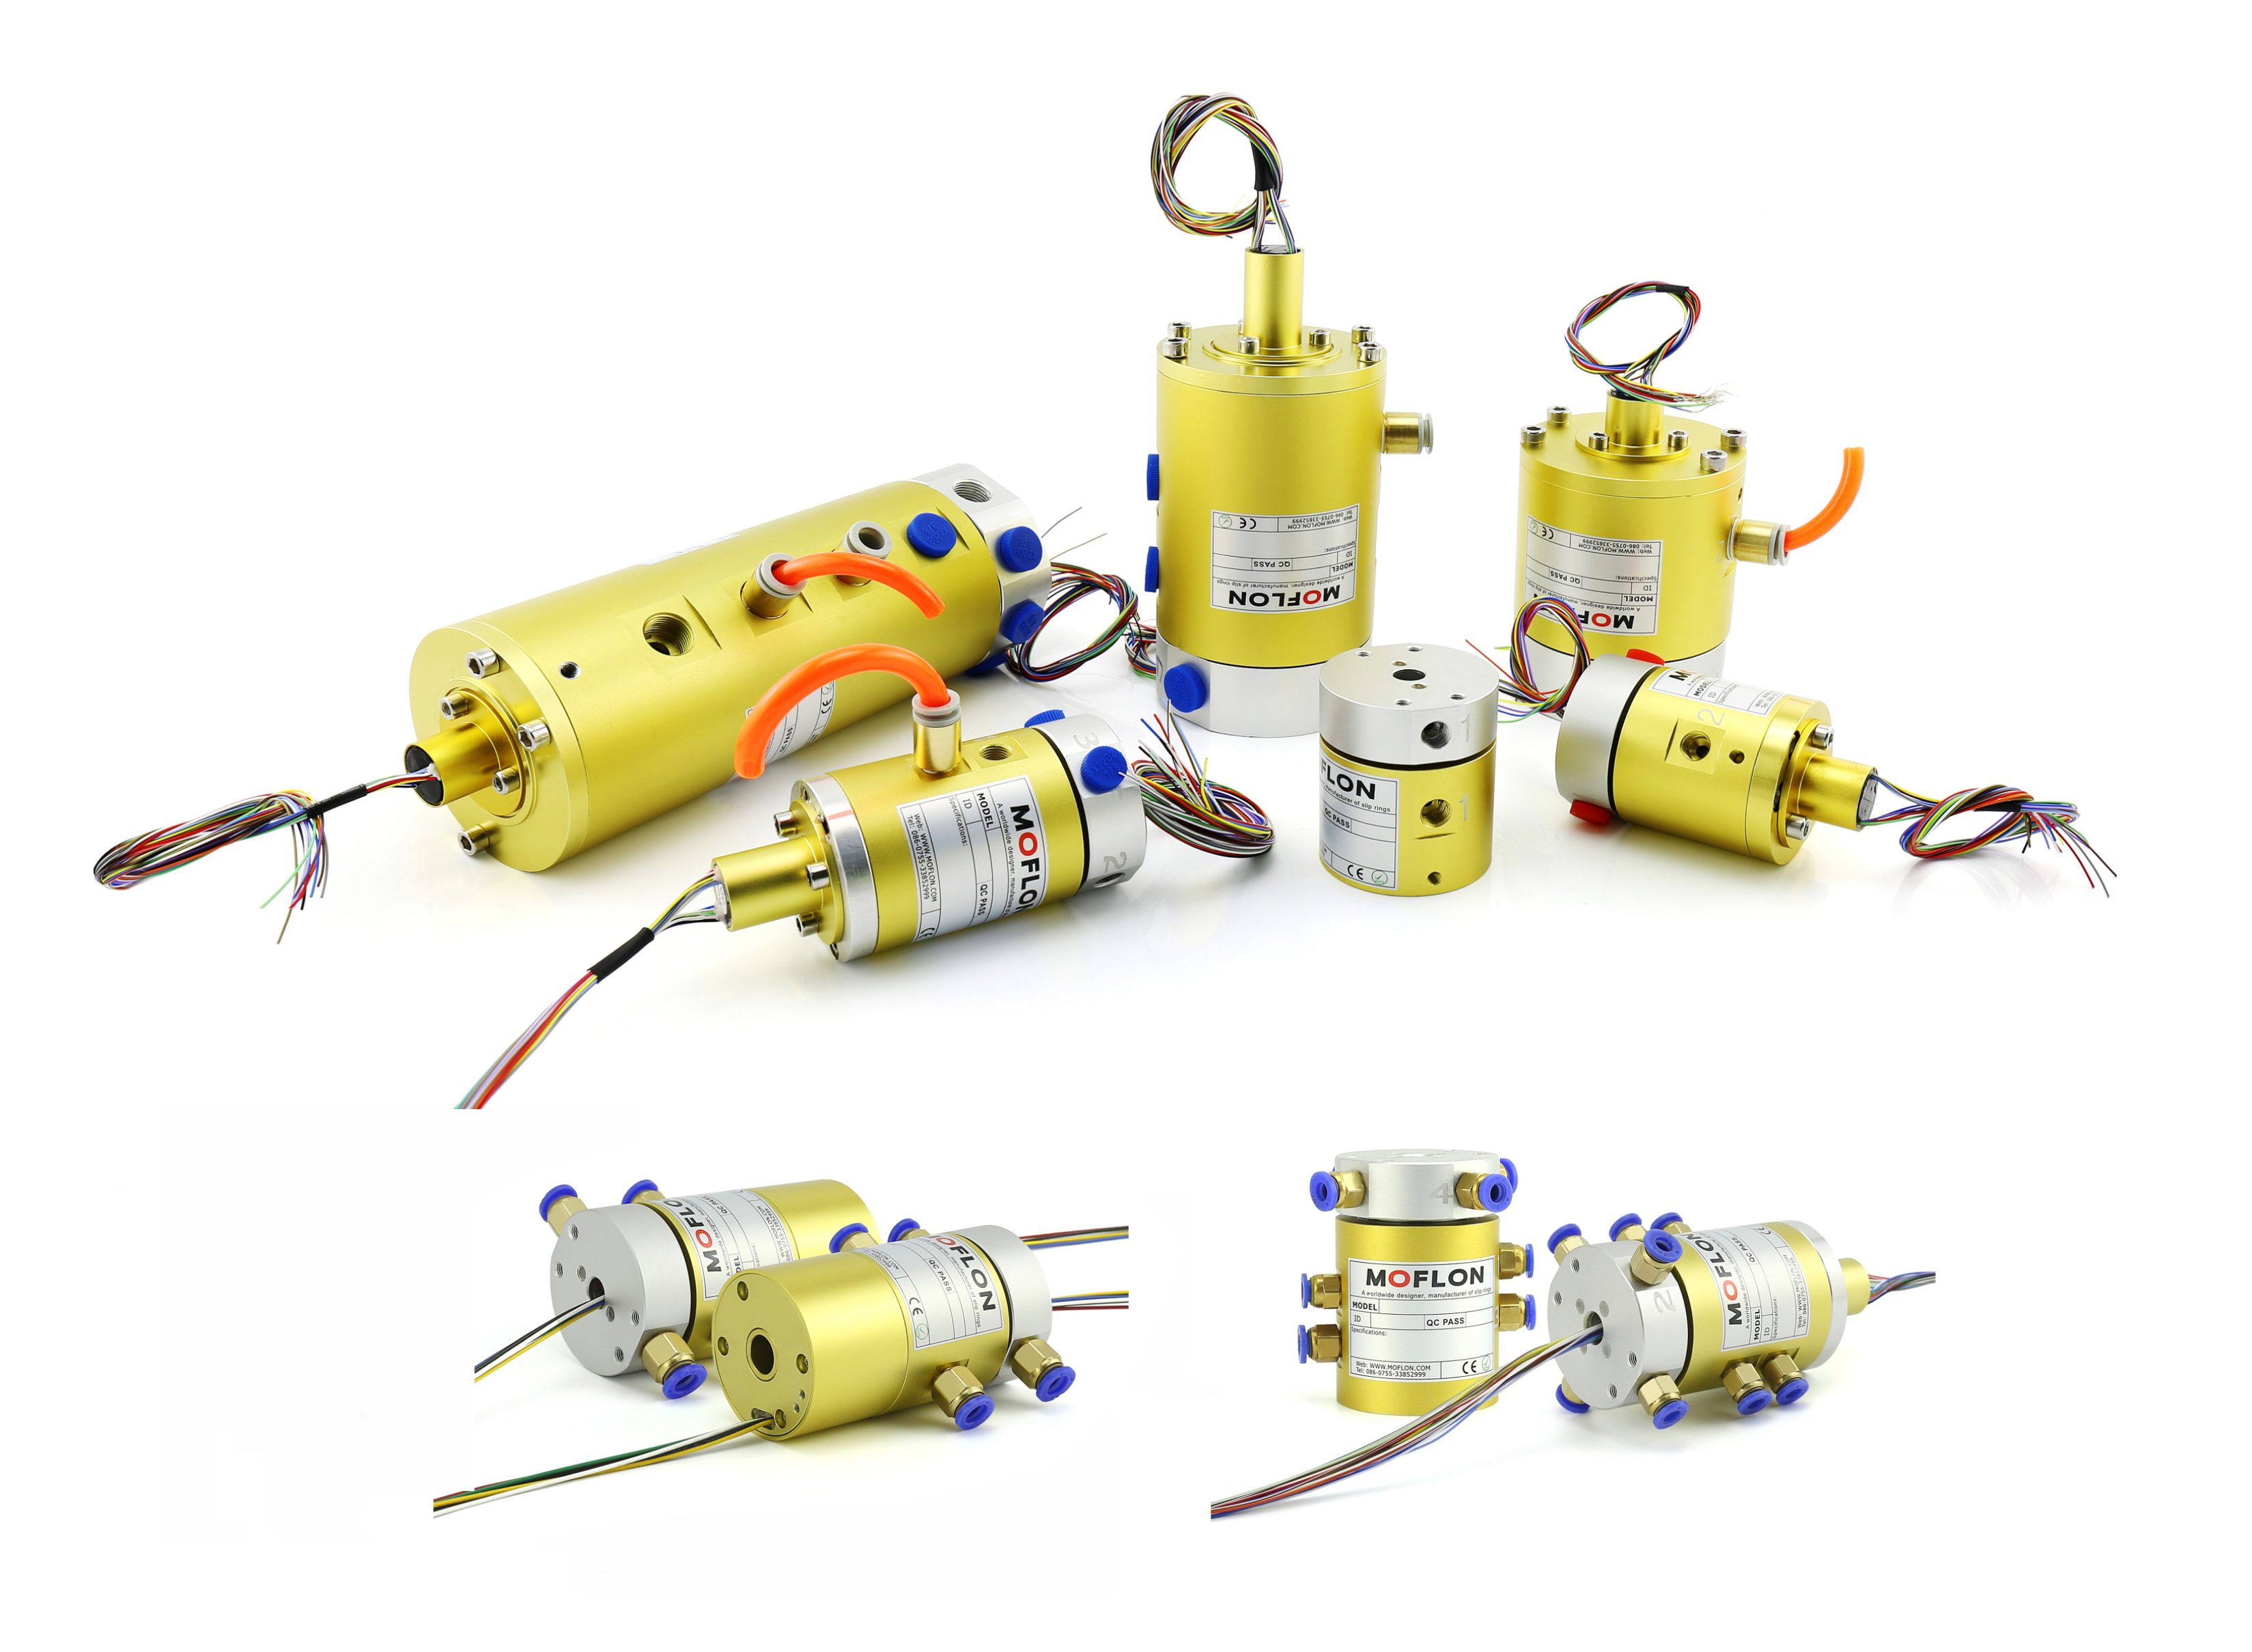
Inside a spinning tool holder, the air that naturally fills every gap and bore starts moving in ways most machinists never think about. At rest, those channels are just passive voids—nothing flows, nothing resists. But once the spindle ramps up to 20,000 or 30,000 RPM, centrifugal force flings the air outward, creating a radial pressure gradient that pushes stale, warm air against the channel walls while pulling cooler air toward the center. The result is a constant, invisible circulation driven purely by rotation, not by any pump or compressor. This self-generated airflow can either carry micro-debris away from critical seating surfaces or trap it in dead zones, depending on how the channels are shaped and interconnected.
That same rotation also changes how heat moves through the tool body. Air may not be a great conductor, but when it’s forced to circulate rapidly through narrow internal passages, it starts behaving more like a fluid heat exchanger. Tiny eddies form near sharp corners and sudden diameter changes, stripping heat from the shank and carrying it toward cooler regions near the front or rear. In practice, this means a tool with well-designed internal air channels can run measurably cooler at high speed than an otherwise identical solid tool, simply because the spinning air is doing quiet work behind the scenes.
What’s less obvious is the effect on chip evacuation and coolant draw. High-speed rotation creates a low-pressure zone at the tool’s tip if internal channels connect to the face or flutes. That pressure differential can actually pull ambient air—or mist, or fine chips—backward through the channel, opposite to the intended coolant flow direction. Designers who ignore this phenomenon end up with tools that seem to breathe in their own waste, while careful channel geometry uses the rotation-induced flow to assist rather than fight the primary cooling stream.
Reading Pressure Drop Curves Like a Field Engineer
A pressure drop curve stops being a line on a screen once you've had to explain a 2-bar loss at three in the morning. Field engineers read these curves backward: start with what the system is doing right now, then trace the slope to find the lie. A clean filter gives you a gentle, almost lazy rise in differential pressure as flow climbs. When that curve starts kicking upward too early, something is choking—maybe a strainer full of rust flakes or a control valve hunting off its seat.
The trick is learning which bend in the curve belongs to the equipment and which one belongs to the problem. Compare today's trace against the commissioning baseline. If the shape holds but the whole line shifts up, you have a restriction that grows with flow—classic filter loading or a partially closed isolation valve. If the curve changes slope, especially at higher flow rates, you're looking at a different beast: cavitation, incorrect pipe sizing, or a pump running too far left on its curve. That distinction saves hours because it separates "clean this" from "shut this down before it eats itself."
Veterans also ignore the absolute numbers for the first few seconds. They watch the curve's stability. A jagged, nervous trace, especially on the discharge side, usually means entrained air or a failing check valve. A smooth but steadily climbing trend across a shift tells you the filter is doing its job—right up until it isn't. Field sense means knowing when to trust a flat line and when to poke a gauge with a screwdriver handle to make sure it is not stuck.
The Materials That Survive Moisture, Heat, and Chemical Exposure
Not every material can hold up when the environment turns hostile. Moisture seeps into microscopic pores, heat accelerates degradation, and chemicals attack molecular bonds. Yet a handful of substances have earned a reputation for standing firm. Take 316 stainless steel, for instance. Its molybdenum content gives it exceptional resistance to chlorides and acids, making it a staple in marine hardware and pharmaceutical processing lines. Then there's PTFE, better known by the brand name Teflon. It shrugs off nearly every solvent, tolerates temperatures past 260°C, and doesn't absorb water at all, which is why gaskets and seals in chemical plants rely on it. For applications needing both toughness and thermal stability, ceramics like silicon carbide and alumina shine — they're inert, hard, and unaffected by prolonged humidity or aggressive cleaning agents.
Polymers often get dismissed as flimsy, but a few break that stereotype. PEEK (polyether ether ketone) combines high tensile strength with resistance to steam, hot oils, and a wide range of acids and bases. It survives continuous use at 250°C, outperforming many metals in corrosive environments while weighing a fraction as much. Similarly, EPDM rubber handles outdoor exposure, ozone, and diluted acids without cracking or swelling, which is why it lines hoses and gaskets in automotive cooling systems. Even glass, when properly formulated as borosilicate, handles thermal shock and chemical attack far better than ordinary soda-lime. Lab glassware and sight windows in reactors depend on that exact property.
Selecting the right material isn't just about picking the strongest option on paper — it's about matching the specific threat. For prolonged UV and salt spray, titanium alloys outperform nearly everything but cost more. For secondary containment or cable jacketing in washdown areas, fluoropolymers like FEP and PVDF offer a practical balance. The key is understanding how moisture, heat, and chemicals interact: wet heat accelerates corrosion, and many chemicals become more aggressive at elevated temperatures. That's why engineers often run compatibility tests under worst-case scenarios rather than assuming a material's generic rating will hold up. In the end, the survivors are the ones with dense, stable structures or self-passivating surfaces that refuse to react.
When a Rotary Union Outperforms a Standard Air Slip Ring
In applications where a single rotating joint must handle both compressed air and hydraulic fluid or coolant, a rotary union often leaves a standard air slip ring far behind. Air slip rings are designed primarily for pneumatic transfer, but their sealing systems can struggle when liquids enter the picture, leading to leaks, pressure drops, or cross-contamination. A rotary union built with dual or multi-passage capability isolates each medium cleanly, maintaining consistent pressure and flow even at higher RPMs or under fluctuating loads. That kind of reliability becomes critical in machining centers, rotary indexers, and packaging lines where downtime from a failed seal costs far more than the component itself.
Another area where a rotary union outshines a standard air slip ring is in high-pressure or high-temperature air service. Many off-the-shelf air slip rings use lightweight seals and compact bearings that work fine for low-demand pneumatic signals or modest air flow, but they fade quickly when the job calls for continuous operation at 150 PSI or temperatures above 80°C. A well-engineered rotary union with hardened sealing faces, balanced mechanical seals, and robust bearing arrangements holds up under these harsher conditions, reducing seal wear and extending service intervals. This makes it the preferred choice for tire curing presses, injection molding machines, and other equipment that pushes compressed air to its limits.
If your equipment cycles frequently or runs around the clock, a rotary union can also provide a longer maintenance-free window. Standard air slip rings often need periodic inspection and seal replacement because their design prioritizes compactness over ruggedness. Rotary unions, especially those with field-replaceable seal cartridges, let you swap out worn components quickly without pulling the entire joint. Over time, the lower total cost of ownership and reduced unplanned stops give the rotary union a clear edge — not because it does one thing dramatically better, but because it handles real-world operating abuse without demanding constant attention.
Pre-Installation Checks That Prevent Most Early Failures
Most early failures can be traced back to a short list of issues that become obvious if you pause before the first screw turns. Confirm the mounting surface is flat and clean, verify every part matches the bill of materials, and compare electrical ratings against the actual supply at the site. A quick scan for bent pins, hairline cracks in housings, or foreign material on contacts will save hours of troubleshooting later.
Environmental conditions usually get less attention than they deserve. Take temperature and humidity readings at the exact install location rather than relying on the building average. If you notice condensation, dust accumulation, or any sign of water intrusion nearby, resolve that before bringing components into the space. Also look at the planned cable routing to make sure nothing will pull on connectors or block ventilation paths once the covers go on.
Before powering anything up, keep the load disconnected and walk through the startup sequence in order. Meter the incoming voltage at the terminals, test ground continuity, and check phase rotation where it matters. These steps take only a few minutes, yet they catch most faults that would otherwise appear as dead-on-arrival units or nuisance trips within the first week.
FAQ
Pay attention to seal material and bearing quality first. A supplier that openly shares torque specs and leak rates is usually more trustworthy than one that only advertises 'low friction'. Ask for a test report at your operating pressure and speed, not just a catalog sheet. Also check whether they offer modular designs, because replacing a worn seal shouldn't mean buying a whole new unit.
Early leakage is almost always tied to misalignment or dry running. If the mating shaft has runout beyond the slip ring's tolerance, the seal lip wears unevenly and air escapes. Many users forget that rotary seals need a thin lubrication film to survive; running them completely dry causes heat buildup and cracking. Installing a proper filter upstream also stops dust from embedding in the sealing surface.
It's possible, but only if the unit was designed as a dual-purpose rotary union. Most standard air slip rings are optimized for one direction, so reversing pressure can flip the seal lip and cause immediate failure. If your process switches between vacuum and compressed air, ask for a bidirectional seal arrangement and keep the pressure differential within the manufacturer's stated limit.
Start by mapping every pneumatic function that crosses the rotating interface, not just the ones you use today. Add at least one spare passage for future tooling or a sensor air purge. If you have vacuum cups that need separate zones, count each zone as its own passage. It's cheaper to buy a slip ring with an unused port than to retrofit a second unit later.
Contacting seals use a physical lip that rubs against the rotor, so they provide a tighter static seal but generate more wear and heat at high speed. Non-contacting designs use a small air gap or labyrinth, which allows higher RPM and longer service intervals but allows a small controlled leakage. Choose based on your duty cycle: continuous high-speed rotation favors non-contacting, while intermittent low-speed indexing can work fine with contacting seals.
For cleanroom environments, standard catalog units rarely meet the low-outgassing and particle-shedding requirements. You'll usually need a variant with specialized grease, hard-coated sealing surfaces, and possibly a purge port to keep contaminants away from the seal. If a supplier doesn't ask about your cleanroom class and chemical exposure, keep looking.
The seal lip can extrude into the gap between rotor and housing, causing sudden torque spikes or complete lock-up. Even if it doesn't fail immediately, overpressure shortens seal life significantly because the contact stress is far beyond design limits. Always install a pressure relief valve upstream, and remember that pressure spikes during valve shifting can exceed your compressor's steady-state reading.
Conclusion
The most dependable air slip ring setups rarely advertise themselves through polished housings; they earn trust at the sealing interface. A perfect running seal prevents moisture ingress and pressure bleed far better than any cosmetic enclosure, especially when a joint spins at high speed and internal channels flex, expand, or develop micro-leaks. Field engineers often skip straight to pressure drop curves because those plots reveal whether a unit will hold rated flow under load or quietly starve the tooling. Materials matter just as much as geometry: seals and wetted surfaces that can shrug off condensation, heat cycling, and aggressive chemicals outlast generic components by a wide margin. In many high-duty-cycle applications, a purpose-built rotary union simply outperforms a standard air slip ring by offering cleaner port separation and lower leakage across the same rotational speed.
Before any of that performance can show up on the floor, however, pre-installation checks do the heavy lifting. Verifying shaft alignment, thread depth, and supply air cleanliness prevents the early failures that often get blamed on the slip ring itself. Once the unit is properly mounted and the pressure curve is logged against baseline, the difference shows up as stable torque, consistent media delivery, and fewer unplanned stops. The best solutions are therefore not defined by a single part number or brand, but by how well the seal, materials, and installation practices work together under real rotational loads. That combined view is what separates a reliable rotational connection from one that only looks good in a catalog.
Contact Us
Contact Person: Xiangpin Li
Email: [email protected]
Tel/WhatsApp: 86 186 1706 8578
Website: https://www.moflon.com