Chinese High-Speed Wire Rod Mills Transforming Steel Production Worldwide
2026-10-12
The global steel industry is witnessing a quiet revolution, and it’s rolling out of China at unprecedented speed. High-speed wire rod mills—once a niche technology—have become the backbone of modern construction, automotive, and infrastructure projects worldwide. But what’s driving this transformation isn’t just volume; it’s precision, efficiency, and a relentless push toward smarter production. At the heart of this shift stands GRM, a name synonymous with cutting-edge mill engineering. From reducing energy consumption to boosting output without sacrificing quality, Chinese mills are rewriting the rules of steel manufacturing. In this post, we’ll explore how these machines are reshaping global supply chains, why speed matters more than ever, and where GRM fits into the future of metal forming.
Speed Records and Precision That Redefine Rolling
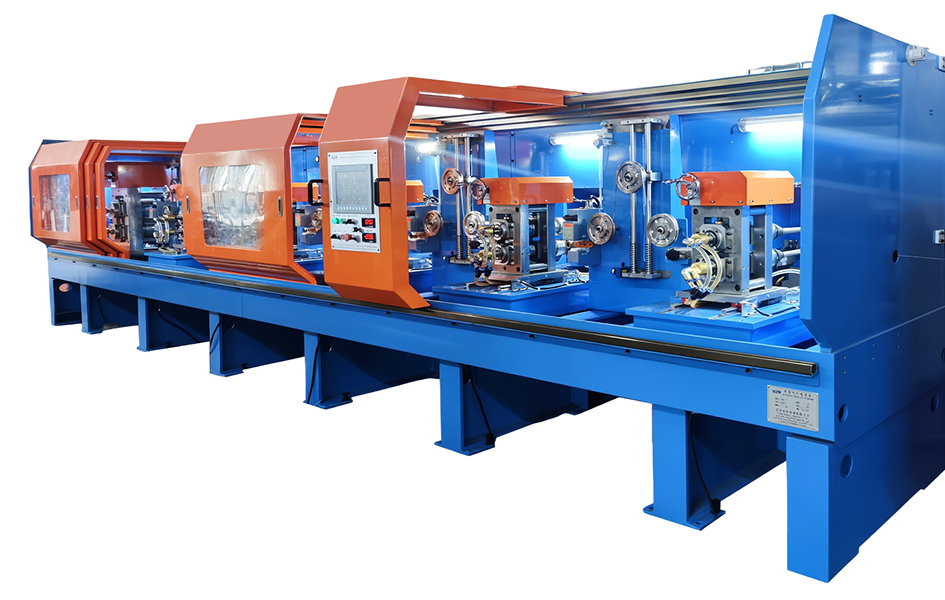
The latest rolling platform hits throughput numbers that were unthinkable a few years ago. Its drive system pairs a high-torque motor with an adaptive feed algorithm, so the line accelerates from standstill to full speed in under two seconds without slipping or jolting. Operators notice the difference immediately: fewer stops, smoother transitions, and a steady stream of finished product that keeps downstream processes fed.
Precision is engineered into every contact point. Rollers are machined to a flatness tolerance of 0.005 mm and mounted on preloaded bearings that eliminate lateral play. That means material thickness stays within ±0.01 mm across the full width, even at top speed. For operators running thin foils or sensitive alloys, this level of control reduces scrap rates and removes the guesswork from setup changes.
What sets this system apart is how speed and accuracy reinforce each other. Rather than trading one for the other, the control software continuously samples roll gap and tension data 400 times per second, making micro-adjustments before deviations become visible. The result is a rolling process that feels stable at record pace — and a finished surface that needs little to no post-roll correction.
How Chinese Mills Slash Production Costs Without Cutting Corners
Walk through any major manufacturing cluster in the Pearl River Delta or along the Yangtze, and the cost advantage becomes visible long before you enter a factory. Suppliers of buttons, zippers, dyed fabric, and packaging sit within a 30-kilometer radius, turning what would be weeks of logistics elsewhere into same-day pickups. This density lets a mill order raw materials in smaller, more frequent batches, slashing warehousing and working capital needs without ever touching product quality. The savings come from speed and proximity, not from downgrading inputs or skipping inspection steps.
Automation in Chinese mills often looks less like a lights-out robot army and more like a careful re-engineering of repetitive tasks. On electronics assembly lines, simple pneumatic arms feed components while skilled workers handle visual inspection and micro-adjustments—a hybrid setup that costs a fraction of full automation but delivers higher first-pass yield. Cross-training operators to run two or three adjacent stations also removes idle time and allows quick rebalancing when orders shift. This approach keeps labor flexible and equipment utilization high, avoiding the hidden cost of over-investment in machinery that would need to be amortized through higher prices or cheaper materials.
Energy and workflow waste are treated with the same rigor as raw material pricing. Mills regularly audit compressed air systems, recover heat from dyeing vats, and schedule power-hungry processes during off-peak tariff windows—cuts that lower utility bills without altering production parameters. Lean tools like single-minute die change and visual kanban have been adapted to local conditions, stripping out waiting time, over-processing, and excess motion. Because these savings are harvested from eliminating waste rather than relaxing tolerances, the finished goods still meet the same specifications, just with a leaner cost structure behind them.
From Construction Steel to Automotive Wire: Versatility in Every Coil
A single coil of steel can end up holding a skyscraper together or carrying signals through a vehicle’s wiring harness. That range starts with the way the material is processed and drawn, allowing mills to tailor strength, ductility, and surface finish without changing the base chemistry dramatically.
On construction sites, the same grade that works for rebar ties and mesh often gets specified for high-tension cable trays or anchor bolts. Switch to automotive use, and the demands shift: tighter diameter tolerances, cleaner surfaces, and consistent elongation become critical for wire that feeds automated bending and crimping machines. Few materials move this easily between such different worlds.
Energy Recovery Systems That Turn Waste Heat Into Profit
Every industrial process bleeds heat into the air, and most plants treat that escaping energy as an unavoidable cost of doing business. Yet a growing number of operators are discovering that the hot exhaust from a furnace, the warm water leaving a cooling loop, or the radiant glow off a kiln can be captured and put back to work. The principle is straightforward: thermal energy that would otherwise dissipate gets routed through a recovery unit—a heat exchanger, an organic Rankine cycle generator, or a thermoelectric module—and converted into electricity, preheated feedstock, or building warmth. What was once a line item for waste disposal becomes a second revenue stream, often with an internal rate of return that surprises even skeptical engineers.
The payoff depends less on the size of the plant than on the temperature and consistency of the waste stream. A cement kiln radiating at 400°C offers far more recoverable exergy than a data center’s tepid exhaust, but even low-grade heat can be lifted with a heat pump or used directly for drying, washing, or space heating. The real differentiator is how the system is integrated. Rather than bolting on a generic unit, successful sites map thermal flows hour by hour, season by season, and design recovery around the specific rhythm of the process. One foundry, for example, feeds stack gases through a waste heat boiler that produces steam for its own mold-making line, cutting fuel purchases by a third while smoothing out the spikes in energy demand that used to trigger peak pricing.
Maintenance and monitoring are where the long-term economics get settled. A heat exchanger that fouls silently will erase its own payback within months, so operators who profit from waste heat tend to treat the recovery equipment as an extension of the production line, not an add-on. Sensors track pressure drop, approach temperature, and output flow, flagging degradation before it becomes a loss. The result is a quieter kind of profit—less visible than a new product launch, but steadier, and increasingly necessary as energy prices swing and environmental rules tighten. For plants that master the details, the waste heat that once vanished into the sky becomes one of the most reliable assets on the balance sheet.
Export Growth and the Shift in International Supply Chains
Export growth used to follow a simple logic: find the cheapest production location, ship components across multiple borders, and assemble goods wherever labor costs were lowest. That model is now under strain. Tariff disputes, pandemic-era border closures, and mounting geopolitical tensions have pushed manufacturers to treat supply chain resilience as a factor equal to unit cost. As a result, export expansion in sectors like electronics and automotive is no longer driven solely by a single dominant factory base but by a patchwork of regional hubs that can each serve nearby demand without relying on fragile long-distance links.
The redrawing of supply chains does not happen uniformly. Some companies move final assembly to Vietnam, Mexico, or India while keeping high-value component production in established locations. Others invest in automation to bring certain steps closer to end markets, not because labor is cheaper but because lead times and inventory carrying costs have become more painful than wage differentials. Countries that once competed mainly on low wages now need reliable electricity, fast customs clearance, and enough skilled technicians to handle increasingly complex tasks. Export growth increasingly tracks those capabilities rather than simple wage arbitrage.
This shift also changes what export statistics mean. A country can report slower growth in final goods exports while its intermediate goods exports boom, as production networks fragment into shorter, more specialized segments. The old assumption that a rising export volume automatically signals a competitive manufacturing sector is less reliable. Instead, success depends on where a country sits within a network that values proximity, redundancy, and the ability to switch suppliers quickly when disruption hits. The new map of trade rewards economies that can plug into multiple regional chains at once.
Smart Automation and Real-Time Quality Control on the Floor
On a busy injection molding line, small thermocouples and pressure transducers embedded in the tooling now sample readings every few milliseconds. A compact edge controller compares those values against acceptable bands and adjusts barrel temperature or clamp force on its own. Operators no longer wait for a scheduled quality check to discover that a batch has drifted out of spec—the line corrects itself while parts are still being formed.
Vision systems mounted above the conveyor do more than spot obvious cracks or short shots. Laser profilers measure critical dimensions on each part and feed that data back to a reference model. When a dimension starts trending toward the upper control limit, the system flags the run and automatically diverts suspect pieces into a quarantine lane. At the same time, it sends a suggested parameter change to the upstream station, closing the loop without a manual stop.
For floor staff, this shifts the daily routine away from repetitive gauging and manual logbooks. They watch exception dashboards that highlight only the machines and molds needing attention, then investigate root causes with complete traceability for every shift. Because the data is stored by serial number and timestamp, a quality dispute with a downstream customer can be resolved by pulling up the exact process signature from that production window.
FAQ
Their combination of high rolling speeds, precision temperature control, and modular design allows mills to switch between product sizes quickly while keeping dimensional tolerances tight. This flexibility has made them attractive to both large integrated plants and smaller regional producers.
Modern Chinese mills often run at rolling speeds above 100 meters per second and use continuous no-twist rolling, which cuts down on cobbles and downtime. Faster billet welding, automated guide adjustment, and quick roll changing can raise output by twenty to thirty percent over legacy lines.
Southeast Asia, the Middle East, and parts of Africa have been the fastest adopters, largely because the mills can be scaled to local demand and paired with electric arc furnaces. Eastern Europe and Latin America are also seeing growth, especially where older Soviet-era or 1980s mills need replacement.
Automation systems handle tension control, loop regulation, and speed cascading across the finishing blocks, so operators spend less time making manual corrections. Some lines now include real-time surface inspection and predictive maintenance alerts, which reduce unplanned stoppages and improve coil consistency.
Cost is a major factor, but not the only one. Chinese suppliers often deliver complete packages that include reheating furnaces, rolling stands, cooling beds, and coil handling equipment, with shorter lead times and easier access to spare parts. This turnkey approach lowers project risk for mills in developing markets.
Newer Chinese high-speed mills typically integrate regenerative burners, waste heat recovery, and variable frequency drives, which lower energy use per ton of wire rod. When paired with scrap-based electric arc furnaces, the overall carbon footprint can be significantly below that of older blast furnace routes.
Yes, many are designed for a wide range of grades, from low-carbon drawing wire to high-carbon tire cord and welding wire. Controlled cooling lines with Stelmor conveyors allow operators to adjust cooling rates, so the same mill can produce everything from soft annealed rod to high-strength cold-heading stock.
Conclusion
High-speed wire rod mills from China are setting new benchmarks that go well beyond raw output. The latest lines run at rolling speeds once considered impractical, yet the dimensional accuracy and surface finish of each coil remain remarkably tight—a combination that forces established producers to rethink their own tolerances. Rather than achieving lower costs through thinner inputs or reduced maintenance, these mills lean on refined pass schedules, longer-lasting roll materials, and tightly controlled cooling paths. What emerges is a product that serves rebar fabricators and automotive component makers alike, often from the same mill floor without extensive changeover. Energy recovery adds another layer: waste heat from the rolling and reheating stages is captured and fed back into plant utilities, turning a traditional cost center into a steady internal revenue stream.
That operational edge is now reshaping international supply chains. Buyers in Southeast Asia, the Middle East, and parts of Africa increasingly source Chinese wire rod not only for price but for consistent metallurgical properties and fewer coil-to-coil surprises. Meanwhile, smart automation on the floor keeps variability in check. Sensors track tension, temperature, and section geometry in real time, and the control system adjusts roll gaps or cooling rates before a single bad ring reaches the laying head. The result is less downgraded stock and faster qualification for demanding end uses. As these mills continue to expand export capacity, the old assumption that high speed means low flexibility no longer holds. Instead, Chinese producers are proving that speed, precision, and sustainability can coexist in a single rolling line, and that shift is quietly redrawing the map of global steel supply.
Contact Us
Contact Person: Rayna
Email: [email protected]
Tel/WhatsApp: 86 -173 1474 6343
Website: https://www.grmrollingmill.com/