Log Saw Cutting Machine Factory: How Advanced Production Lines Deliver Consistent Cutting Performance
2026-09-23
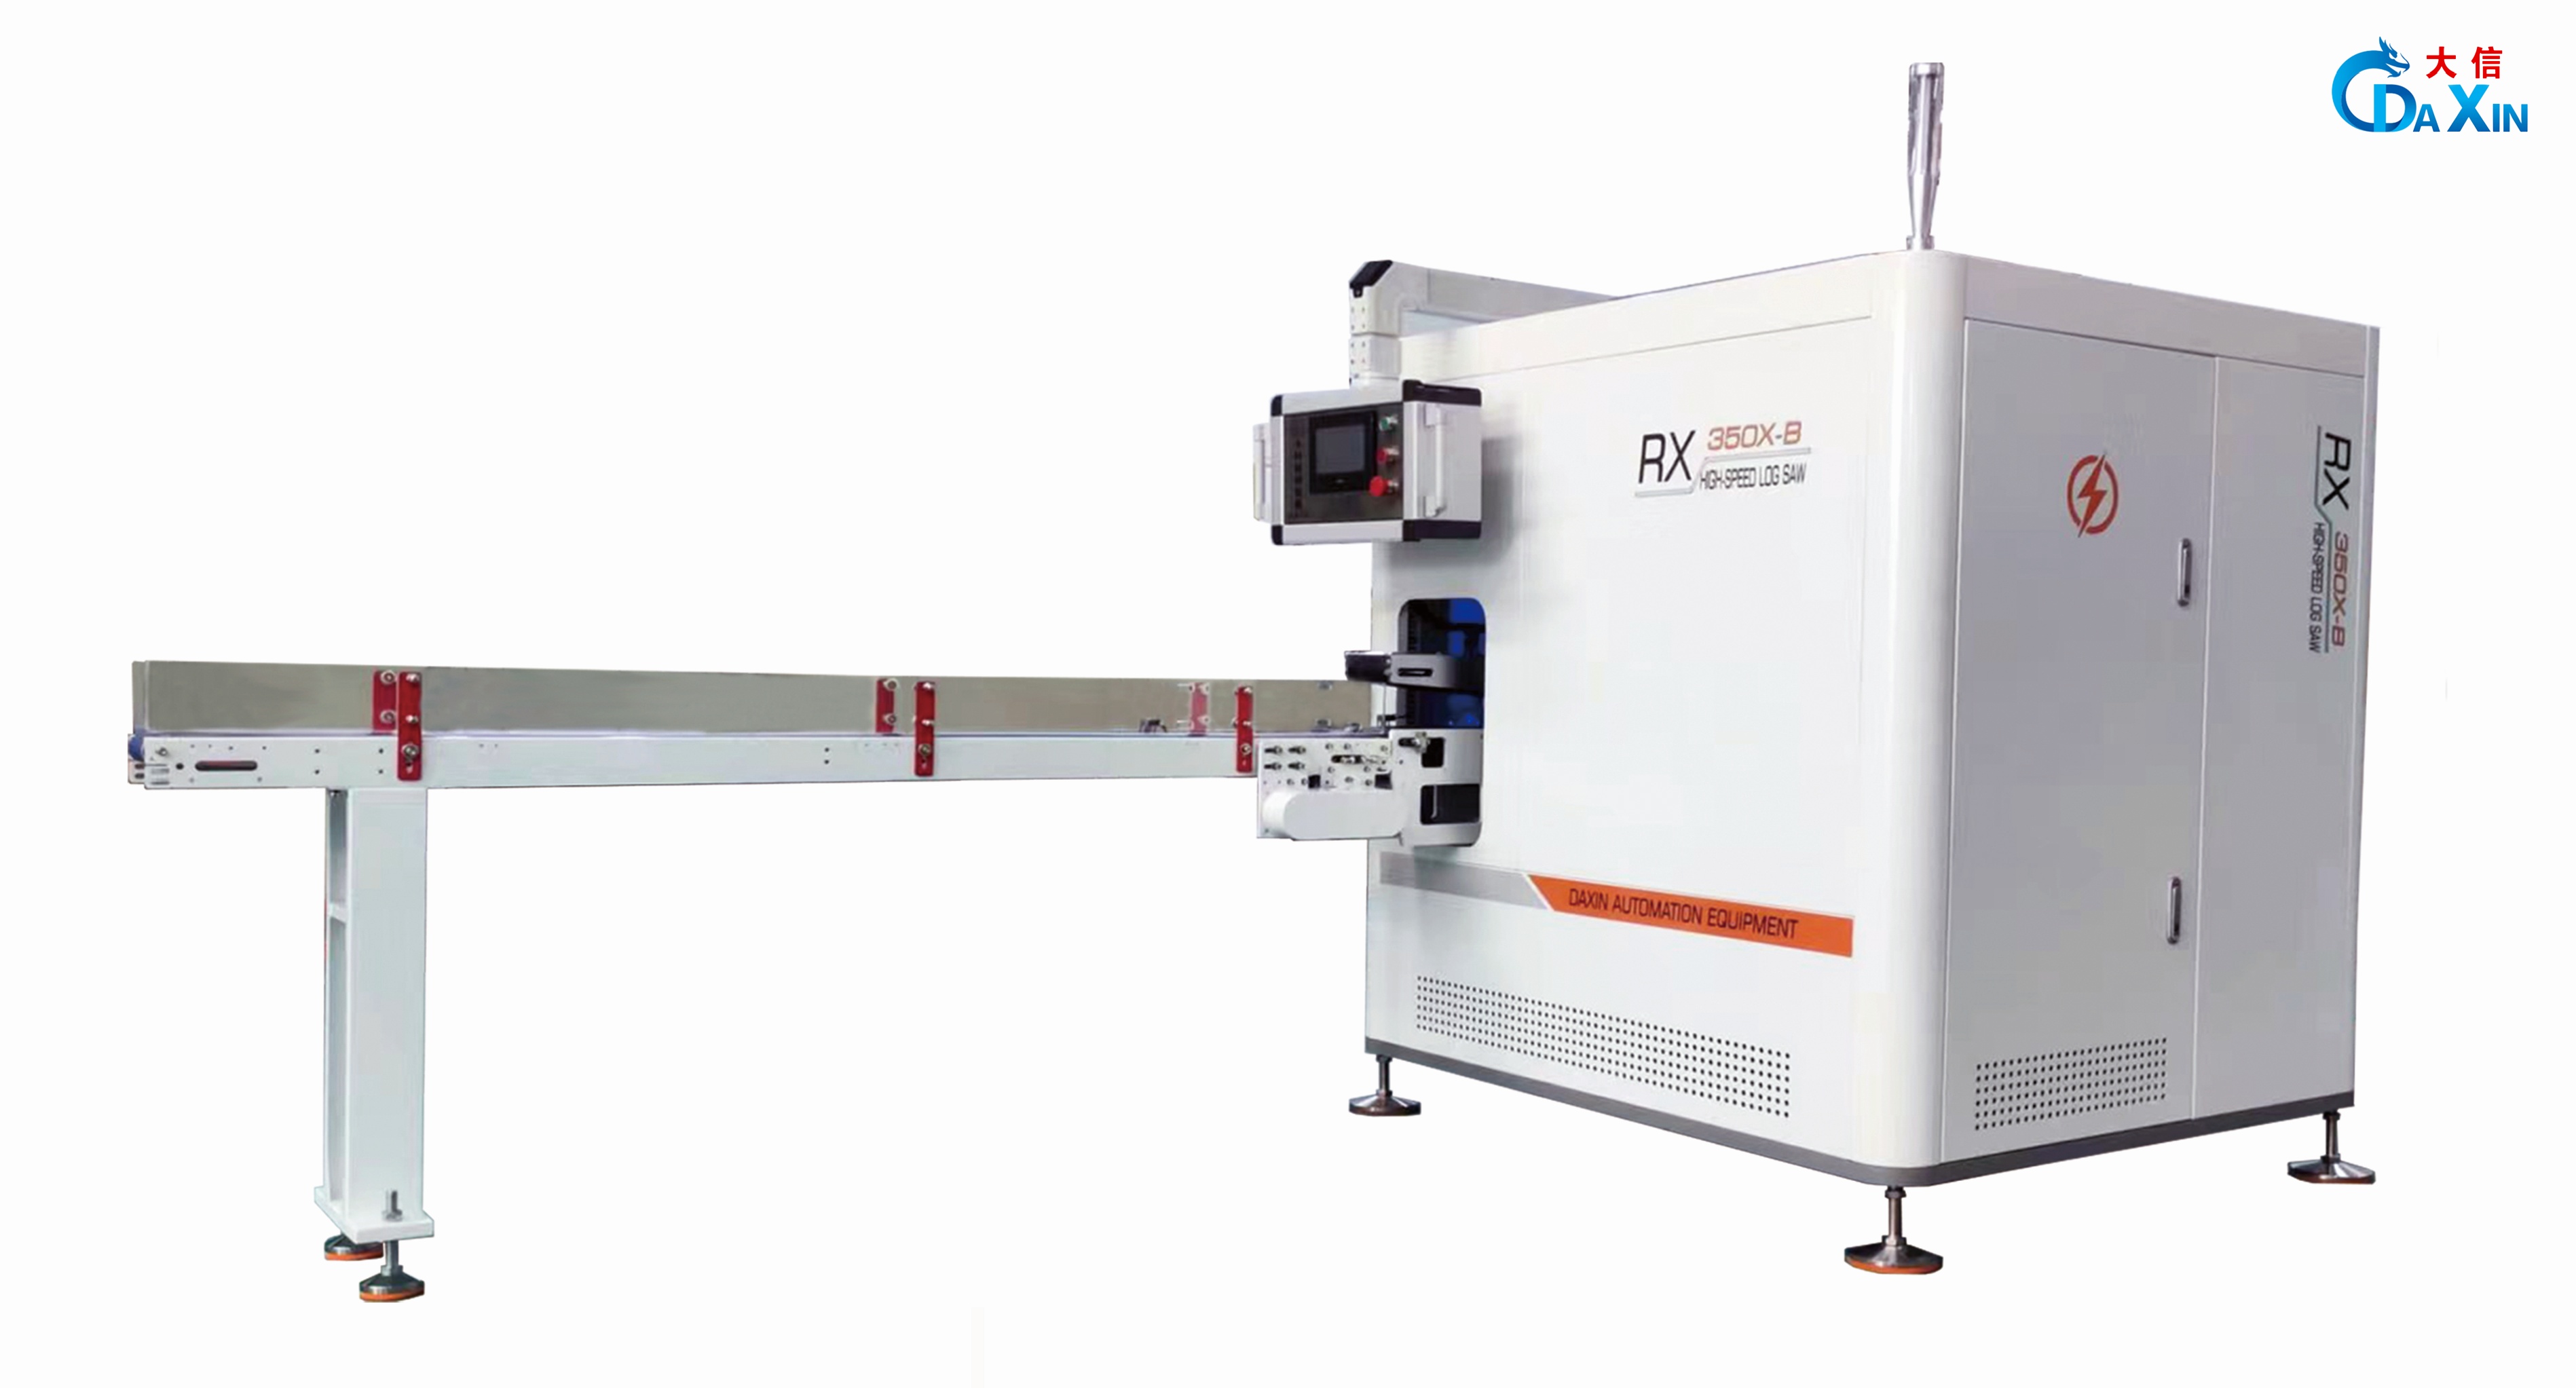
A split-second inconsistency in a log saw cutting machine can ripple through your entire production line—wasted timber, botched dimensions, and frustrated operators. Yet most factories still treat cutting precision as a matter of luck. At DAXIN, that luck has been engineered out. Step inside their advanced production lines and you’ll see why consistent cutting performance isn’t a promise—it’s a measurable output, built into every machine before it leaves the floor.
Precision Machining That Sets the Baseline for Every Cut
Every rotation of the spindle carries a quiet promise: the tolerance you cannot see is the tolerance you will feel. Our machining process begins long before metal meets tool—it starts with the calibration of intent. We do not chase micron-level accuracy as a metric; we treat it as a physical law, like gravity or thermal expansion, and design our fixtures, toolpaths, and cutting parameters to obey it without negotiation.
The result is a baseline that other shops struggle to match on their best day. Burrs are not polished away after the fact; they are engineered out of existence through cutter geometry and feed rates that anticipate chip formation. Surface finishes arrive pre-verified by in-process probing, not by a final inspection that catches what went wrong. This is not about holding a number on a drawing—it is about making every cut feel inevitable, as if the part always wanted to be exactly this shape and we simply removed everything that was not it.
What sets this baseline apart is that it does not fluctuate with operator mood or machine temperature. Repeatability is baked into the workflow: tool wear is compensated in real time, thermal drift is mapped and offset before it can skew a dimension, and each setup references the same certified datum structure. When you receive a part from this line, you are not hoping it meets spec—you are holding a physical argument for why spec was the wrong word to begin with. Precision, at this level, is not a feature. It is the floor.
Automated Controls That Keep Blade Paths Predictable
A predictable blade path isn’t a happy accident—it’s the result of control loops that read wind speed, rotor torque, and vibration forty times a second, then nudge pitch actuators before a gust can twist the load. On newer turbines, these loops also learn from past shear events, so the blade’s sweep stays within a narrow corridor instead of wandering into stall or flutter.
What separates a calm machine from one that hunts is how well the controller handles partial sensor failure. If an anemometer ices over, the system switches to a model-based estimate of inflow angle and keeps commanding blade angles that hold the tip-speed ratio steady. The result is a path that looks boring from the ground—and that’s the point.
Maintenance crews notice the difference in bearing wear and pitch motor heat. Because the blades aren’t constantly correcting for avoidable deviations, the hydraulic accumulators hold pressure longer and the root bushings don’t oval out. Boring blade paths, it turns out, are the cheapest ones to run.
Heavy-Duty Frames Built to Resist Vibration and Flex
The frame starts with thicker cross-sections and gusseted corners, which do most of the work when equipment shakes or twists under load. Instead of relying on a single plate or weld, the structure spreads stress across multiple contact points so no single joint takes the full brunt. That approach keeps alignment stable even when motors ramp up or the floor underneath isn’t perfectly level.
Welds are placed where the metal naturally wants to flex, not just where it’s easiest to reach during assembly. Diagonal bracing and ribbed channels stiffen the center span, while bolted connections are torqued in a sequence that pulls the frame into a slight preload. This removes the micro-movements that normally lead to cracks around bolt holes and mounting feet.
For operators, the result is less downtime spent re-tightening fasteners and fewer alignment checks after heavy cycles. The frame stays put because it was built to move with the vibration, not against it, absorbing energy before it reaches sensitive components.
Inline Gauging That Catches Deviation Before It Compounds
Inline gauging doesn't wait for a finished part to reveal a problem. It measures critical features in real time as the workpiece moves through each station, flagging the smallest drift in diameter, flatness, or position before that deviation can influence downstream operations. This immediate feedback keeps the entire process aligned with the nominal spec, rather than letting small errors stack up into a costly reject.
Traditional post-process inspection often finds a defect after an entire batch has been machined or assembled. By then, the root cause has already multiplied across dozens of parts, forcing rework or scrap. Inline gauging disrupts that reactive pattern by catching the first out-of-tolerance trend, so operators can adjust tool wear, thermal drift, or clamping pressure while the correction is still cheap and localized.
The real advantage emerges in long production runs where subtle shifts are easy to miss until they compound. With inline gauging data streaming continuously, engineers see deviations as they start, not as a final histogram of failures. That shift from end-of-line detection to in-process prevention turns quality from a gatekeeper into a control loop that protects throughput and margin at the same time.
Full-Load Testing with Actual Logs, Not Just Spec Sheets
Spec sheets give you peak numbers under ideal conditions, but they rarely survive contact with a production workload. When you push a system to its limits with real traffic, the logs reveal behavior that no benchmark can predict: memory fragmentation patterns, lock contention spikes, and the occasional third-party API that decides to stall for exactly 400 milliseconds. Running full-load tests against actual log streams—not simulated data—forces those hidden weaknesses to the surface before your users find them.
The process starts by capturing logs from a live environment during a known busy period, then replaying them at maximum throughput against a test cluster. This isn't about hitting a magic number of requests per second; it's about watching how the system's internal timing shifts under sustained pressure. Log timestamps become your primary diagnostic tool. A single slow database query might show up as a two-second gap in one thread while a hundred other requests queue behind it. That's the kind of detail a spec sheet will never mention.
Eventually, you learn to trust the logs more than the marketing materials. A server that handles 10,000 concurrent connections in a vendor's whitepaper might crumble at 3,000 when the requests are messy, irregular, and full of real-world cruft. Full-load testing with actual logs gives you a measurable, reproducible way to separate what the hardware claims from what it can actually deliver when everything is on the line.
Same Clean Edges from Morning Shift to Late Night
Blades that still bite clean at 11 p.m. don’t happen by accident. The edge geometry is set once, then held to a tolerance most shops won’t bother with, so the first pass and the last pass feel like the same tool.
Long days expose weak points fast. Here, the cutting angle stays consistent because the blade seat and guard are machined as a matched pair, not snapped together from a bin of near-enough parts. No drift, no drag, no mid-shift touch-ups.
That means the 6 a.m. lineup and the late-night cleanup crew are working with the same standard. It’s not a fresh edge for the morning crew and a tired one for night shift. It’s the same clean line, hour after hour.
FAQ
Instead of relying on manual adjustments, the production line uses CNC-machined guide rails and laser-aligned blade mounts. Each unit undergoes a 47-point alignment check before it leaves the floor, and the cutting tolerance is verified on three different wood densities.
Servo motors with closed-loop feedback control the blade and carriage independently. The system samples speed 200 times per second and corrects deviations within 0.02 seconds, so even dense hardwoods are cut without stalling or burning.
Automated log decks with weight sensors and laser diameter scanners adjust roller pressure and feed speed in real time. This prevents off-center cuts and keeps the blade engaged at a constant angle, regardless of log taper or bark thickness.
Yes, the modular frame design lets us swap saw heads, conveyors, and outfeed tables while keeping the same calibrated mounting points. Each custom configuration is run through a digital twin simulation before production, so performance parameters are locked before welding begins.
The frame uses stress-relieved steel and the blade arbor has an active cooling jacket. Temperature sensors on the blade guide adjust tension automatically, and the control system applies a thermal compensation curve learned from 10,000 hours of run data.
Steel for the frame is tested for hardness and grain structure at the mill, and linear rails are inspected with a coordinate measuring machine to within 0.005 mm. Only lots with full traceability documents are released to the welding bays.
A well-designed line reduces unit-to-unit variation, which means the machine you receive will match the demo unit's performance. It also shortens lead times and lowers the chance of hidden defects because each station has built-in error proofing.
All models share the same control architecture and calibrated tooling fixtures. When a new size is introduced, the production team uses a master reference log and a set of go/no-go gauges to verify that cutting force, vibration, and kerf width fall within the same narrow bands.
Conclusion
At the core of a log saw cutting machine factory is an almost obsessive focus on repeatability. Machining centers that turn out spindles, carriage rails, and blade mounts hold tolerances far tighter than most general fabrication shops would bother with, and that precision sets the baseline for every cut. Once the mechanical foundation is right, automated controls take over the motion. Servo-driven feed systems and closed-loop blade positioning keep the cutting path predictable even as log diameter, species, and moisture content shift through the day. The frame does a lot of invisible work too. Thick castings and heavily ribbed steel weldments add mass where it matters, absorbing the vibration and flex that would otherwise show up as rough edges or off-square ends on the output side.
Inline gauging is what keeps small errors from becoming big ones. Right after the cutting head, measurement stations check kerf position, squareness, and edge finish continuously, adjusting feed speed or blade offset before any deviation has a chance to compound. The factory also refuses to rely on spec sheets alone. Every saw goes through full-load testing with real logs, complete with knots, bark, and uneven moisture. That is where feed hesitation, blade wander, and frame movement show up in ways a CAD model never predicts. The payoff is consistency. Morning shift or late night, the cut edges look the same, and the operator is not compensating for a machine that drifts as it warms up.
Contact Us
Contact Person: Sam Xie
Email: [email protected]
Tel/WhatsApp: 86-18938538530
Website: https://www.daxin321.com/