Rubber Mixing Mill Factory: How Modern Production Lines Deliver Consistent Compounds
2026-08-27
Consistency is the hidden currency of rubber manufacturing—without it, even the best formulations fail on the production floor. As modern mixing mill lines evolve, factories that master tight tolerances and repeatable shear forces are winning long-term supplier contracts. At SFC, we’ve watched this shift firsthand, and in this post we break down the engineering details behind mills that deliver the same compound batch after batch.
Why Precise Ingredient Dosing Is the First Step Toward Identical Batches
Every batch starts with the belief that small deviations won't matter. A few extra grams of flour, a splash more water, a half-second hesitation on the scale—these feel harmless in the moment. But the moment you scale that recipe from a test kitchen to a production line, those micro-decisions become the difference between a product customers recognize and one they quietly stop buying.
Precise dosing is less about perfectionism and more about trust. When each ingredient is measured with the same care as the first batch, you're not just repeating a recipe—you're repeating the conditions that made it work. Ovens, mixers, and ambient humidity all fluctuate; the one variable you can truly control is what goes into the bowl. Lock that down, and every subsequent batch inherits the same starting point, the same chemical reactions, the same crumb structure, the same mouthfeel.
The alternative is a quiet drift. Batch three is a little denser. Batch seven browns faster. By batch twelve, the color is off and someone finally asks why. Dosing precision catches that drift before it leaves the mixing room. It turns a recipe from a hopeful suggestion into a repeatable instruction—and that repetition is what brands are built on.
The Role of Closed-Loop Temperature Control in Hitting Target Mooney Viscosity
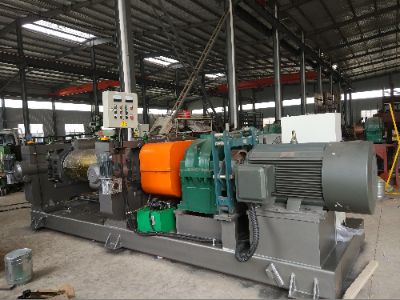
In rubber compounding, Mooney viscosity is highly sensitive to temperature. Even a few degrees of drift during mixing can shift the measured viscosity enough to push a batch outside the target range. Closed-loop temperature control continuously compares the actual stock temperature against a setpoint and adjusts heating or cooling in real time. This keeps the compound within the narrow thermal window needed for repeatable viscosity readings.
The closed-loop approach also accounts for shear-induced heat, which changes with rotor speed, fill factor, and formulation. By feeding temperature data back to the controller and modulating water flow, steam, or rotor speed accordingly, the system compensates for these dynamic conditions. That reduces the need for manual corrections and lowers the risk of over-masticated or under-masticated batches.
When a specific Mooney range is required, closed-loop control turns temperature from a source of variation into a managed variable. The payoff is tighter lot-to-lot consistency, fewer rejected batches, and more predictable downstream processing such as extrusion and molding. Hitting the target Mooney viscosity ultimately depends less on post-mix adjustments and more on holding thermal stability from the very start of the mix cycle.
Replacing Periodic Lab Checks with Inline Sensors That Never Sleep
Traditional lab sampling hinges on grabbing a bottle or pulling a side stream every few hours, which leaves long blind spots between snapshots. Inline sensors replace that intermittent practice by riding directly in the process line and measuring the actual stream continuously. A drift in pH, a slow climb in viscosity, or a shift in dissolved oxygen shows up as it develops, not when a report finally lands after the batch has already moved on. Operators see the real-time signal at the line, without the delay of sample transport, preparation, or bench analysis.
The switch also removes hidden failure points that come with periodic checks. Grab samples can be non-representative, degrade in transit, or get mislabeled. Reagents expire, glassware gets dirty, and lab workload creates queues. Inline sensors stay in contact with the product under true process conditions—temperature, pressure, flow, turbulence—so the measurement reflects what is actually happening inside the pipe or vessel. Calibration can be tracked automatically, and threshold alarms can feed directly into control loops instead of sitting in a logbook until someone reads it.
For plants running around the clock, the biggest gain is continuous confidence. A sensor that never sleeps builds a dense record across every shift, making it possible to spot multivariate trends and schedule maintenance before the process drifts out of spec. Quality control stops being a gate at the end of production and becomes a living part of process control. The lab still earns its keep as a reference for method validation and complex troubleshooting, but routine release decisions no longer depend on a sample that aged before it reached the bench.
How Continuous Cooling and Homogenizing Eliminate Batch-to-Batch Drift
Drift between production runs often starts with thermal history. When a melt cools unevenly, the resulting solid carries microscopic compositional gradients that are nearly impossible to reverse downstream. Continuous cooling keeps the entire cross section on the same trajectory, removing the random nucleation fronts that typically separate one batch from the next.
Homogenizing then does the heavy lifting at the atomic level. Instead of relying on a fixed soak time that may or may not match the incoming structure, the process is tuned to the actual cooling curve of each run. This closes the gap between nominally identical batches, so the final properties no longer depend on which day the material was cast.
The result is a predictable baseline. Operators stop compensating for invisible variability and can focus on adjustments that matter, while downstream steps receive a more uniform starting condition.
When Production Data Starts Tuning the Mixing Recipe on Its Own
The mixer doesn't wait for a supervisor to notice drift. Torque sensors, temperature probes, and inline viscosity meters feed a live stream of numbers into the control system, and the recipe shifts by small increments every few seconds. A batch that would have run too stiff at 10 a.m. gets a tiny water adjustment by 10:04, not after a lab test comes back half an hour later. The operators still watch the screens, but the first move now comes from the data.
What changes is not just speed but the definition of a recipe. Instead of a fixed list of kilograms and minutes, it becomes a target envelope: keep the final slurry within this rheology band, and let the system pick the path. Raw material variation, ambient humidity, even a worn impeller blade all show up as signal, and the loop compensates before the product drifts out of spec. Over time, the accumulated adjustments reveal patterns that no single engineer would have written into the original procedure.
That quiet handover of authority is the real shift. It works well on days when the data is clean and the model's boundaries are respected. But it also demands a different kind of trust: knowing when the system's self-tuning is improving the mix, and when it is quietly learning the wrong lesson from a poorly calibrated sensor.
A Full Digital Record for Every Compound: From Raw Material to Shipping
Every batch receives a digital thread the moment raw materials are logged at intake. Supplier lot numbers, purity profiles, storage temperatures, and handling notes are captured directly, not transcribed later from a clipboard. That same thread then follows the compound through every weighing, reaction, purification, and analytical test, so by the time a container leaves the shipping dock, the record shows exactly which raw material source fed into which step and under what conditions.
Because the record is built as a time-stamped chain of events, it resists the silent edits that paper logs and shared spreadsheets allow. Each handoff appends a new block of data rather than replacing the old one. A chemist can pull up a batch from six months ago, compare its impurity profile against today's run, and see where the deviation started, often before a product fails specification. The same continuity extends outward: when a shipment arrives at a customer site, the receiving team can verify that the container matches the documented chain from raw material to finished compound, without needing to request archived files or wait for a quality review.
That kind of completeness changes how teams handle investigations and audits. Instead of hunting through binders or email attachments, they follow the compound's digital path backward from any point, whether it's a raw material lot, a reactor batch, or a shipped vial. The record carries instrument readings, operator decisions, and even environmental conditions at the time of processing, so root-cause analysis becomes a matter of reading the sequence rather than reconstructing it from memory. Downstream, it means fewer duplicate tests, less rejected material, and confidence that every compound leaving the facility carries its own verifiable story.
FAQ
Modern lines rely on closed-loop control over rotor speed, nip gap, and cooling water flow, so each batch hits the same shear history instead of depending on an operator's feel.
Tight temperature regulation prevents premature scorch and keeps viscosity stable during mastication, which means fillers and curatives disperse the same way from one batch to the next.
Automated feeding systems weigh and add ingredients in a fixed sequence, while programmable recipes adjust mill parameters in real time, removing the drift that manual adjustments cause.
Incoming rubber, carbon black, and oils pass through viscosity and moisture checks, and any lot that falls outside the spec is quarantined before it can reach the mixing line.
Yes, quick-change chutes, dedicated drop zones, and purge batches between recipes let a single line switch from EPDM to NBR or SBR compounds with minimal residue carryover.
Predictive vibration analysis on roll bearings, scheduled regrinding of roll surfaces, and daily checks of nip gap alignment prevent the slow mechanical wear that silently changes mixing intensity.
Sensors track torque, batch temperature, and energy input during mixing, and the system flags any cure that deviates from the reference curve before the batch is dumped.
Poorly dispersed carbon black or silica creates hard spots that lead to uneven extrusion, weak tensile properties, and higher reject rates in molding or calendering.
Conclusion
Getting identical batches out of a rubber mixing mill starts long before the rotors turn. The first weight on the scale matters as much as the final sheet off the mill, and modern lines treat dosing as a closed system rather than a manual routine. Operators no longer rely on scoop counts or visual checks; gravimetric feeders and loss-in-weight hoppers fine-tune every ingredient to within a fraction of a percent, because even a small drift in carbon black or oil throws off dispersion and cure kinetics downstream. Once mixing begins, closed-loop temperature control takes over. Instead of reacting to a hot batch after it has already scorched or under-mixed, the control system reads rotor and chamber temperatures in real time and adjusts cooling water, ram pressure, and rotor speed to hold the compound inside its target Mooney viscosity window. This matters because Mooney is not just a lab number; it is the fingerprint of how the rubber will process later, and hitting it consistently means less rework at the extruder or calender.
What used to happen only in periodic lab checks now happens continuously with inline sensors that monitor viscosity, dispersion, and temperature without ever pausing the line. These sensors flag a drifting batch while it is still correctable, not after it is already packed and shipped. Downstream, continuous cooling and homogenizing remove another hidden source of batch-to-batch drift. A batch that sits too long at high heat after discharge can continue crosslinking or lose plasticizer distribution, so modern lines move the stock through forced-air or water-cooled conveyors and into homogenizing units that equalize temperature and filler distribution before the compound is stacked. The process does not stop at the mill; production data feeds back into the recipe. When the system sees that certain combinations of fill factor and ram pressure produce a narrower viscosity range, it adjusts the next cycle automatically, tuning the formula around the measured result instead of waiting for a monthly review. Every adjustment, every sensor reading, and every raw material lot lands in a full digital record that follows the compound from inbound polymer to outbound shipping, so if a customer ever questions a batch, the answer is not a memory but a traceable, time-stamped history.
Contact Us
Contact Person: Chen Zhengwei
Email: [email protected]
Tel/WhatsApp: +86-13963975727
Website: https://www.sfcrubbermachine.com